GN Separation, a professional vibrating screen manufacturer, has just shipped a custom 5-deck stack vibrating screen to an overseas customer. The unit brings a high-efficiency, space-saving screening solution to their demanding solids processing operations. Built for rigorous industrial duty, this multi-layer machine tackles three common pain points at once: limited site space, high throughput demands, and precise material classification.
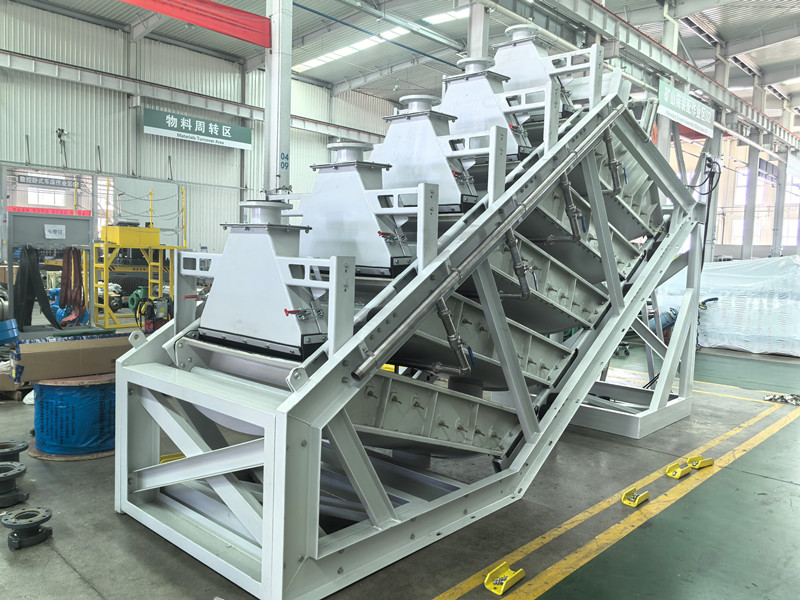
The screen box is driven by a mature dual-motor self-synchronization principle, delivering stable, consistent linear motion across the entire assembly. The result is steady, continuous screening even under long-term industrial load. Unlike traditional single-layer vibrating screens that need multiple machines to complete multi-stage classification, this 5-deck design folds every screening stage into one compact unit. It expands the total screening area, lifts processing capacity dramatically, and occupies minimal floor space — a clear win for factories working within tight layouts.
Energy efficiency and low maintenance sit at the heart of the stack vibrating screen series. The upgraded vibration system cuts power consumption and dynamic load during operation, supporting energy-saving, high-yield production. Premium polyurethane screen panels add another layer of value: they offer excellent elasticity and wear resistance, and help prevent material blinding and screen blockage in fine powder and particle screening.
Configuration flexibility is built in. Each single-layer screen box can hold two to three panels, so the machine adapts easily to different separation requirements. All panels are secured with pull-bolt components, which makes disassembly, replacement, and routine maintenance quick and simple. That user-friendly design shortens equipment downtime and keeps later-stage maintenance costs low.
Durability is never an afterthought for overseas deployment. Every unit receives professional sandblasting followed by heavy-duty anti-corrosion coating to resist oxidation and corrosion. Material contact surfaces get an extra layer of high-performance polyurea resin that withstands abrasion and chemical erosion, extending service life even in harsh environments.
At the core, the vibration system pairs with internationally recognized Martin or OLI vibration motors. Their proven reliability and long trouble-free running time combine with the equipment’s robust integral structure to support 24-hour continuous operation — meeting the high-intensity demands of mining, industrial processing, and environmental treatment alike.
This delivery reflects how GN Separation approaches every project as a professional screening equipment supplier. We never force a one-size-fits-all solution. Instead, we study each customer’s material characteristics, capacity requirements, separation standards, and site conditions, then configure the most suitable layer structure, screen mesh specification, and surface protection scheme.
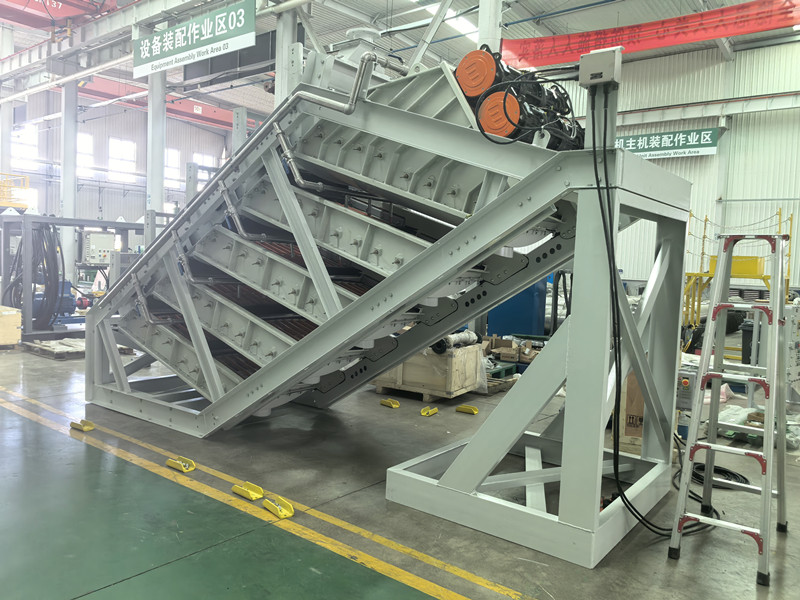
With a compact footprint, high screening efficiency, large processing capacity, energy saving, and low maintenance, the GN stack vibrating screen has become a preferred choice for fine-grained material screening worldwide. Looking ahead, GN Separation will keep advancing solid-liquid separation and screening technology — delivering reliable, efficient, customized industrial solutions to clients across mining, environmental protection, and industrial manufacturing.