Monthly Archives: November 2026

GN High Frequency Stack Vibrating Screen for Domestic Mining Company

GN Separation recently delivered its high-frequency stack vibrating screen to a local mining company, rolling out a dedicated screening solution for fine-grained mineral processing.

This screen integrates the compact structural advantages of stack screening equipment and the separation performance of high-frequency fine screens. It is purpose-built for fine material classification, wet screening and dewatering, addressing common processing challenges in the mining sector.
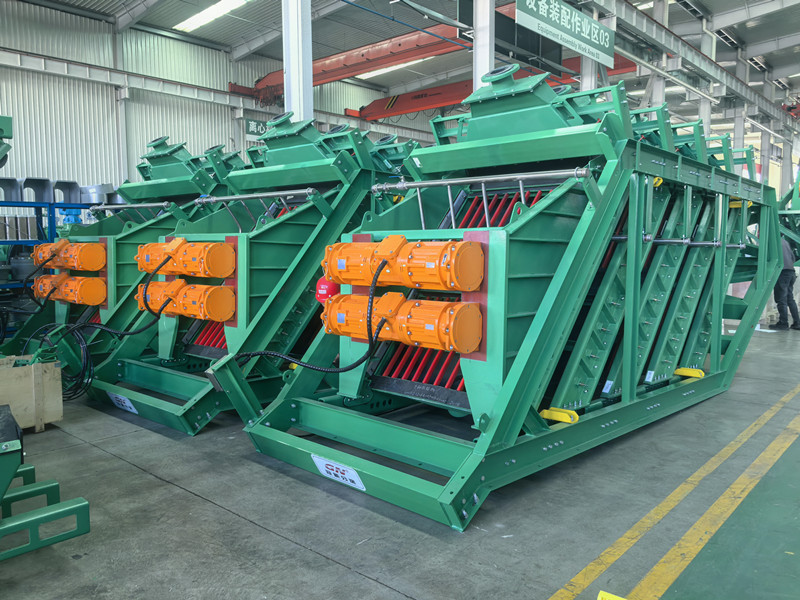
2026.11.11 High Frequency Fine Screen

Most conventional vibrating screens only have one screening deck. In contrast, the GN stack vibrating screen adopts a multi-deck design. Users can select 2 to 5 screening layers based on site layout and process requirements. Multiple screening surfaces are integrated into one unit, saving valuable floor space while offering flexible processing capacity. It is ideal for mineral processing, coal preparation and other scenarios requiring fine particle separation.

The highlight of this equipment is its self-developed vibration system, which adopts the two-degree-of-freedom resonance principle. Two imported vibration motors act as a single vibration source to drive the whole machine and produce stable linear vibration. The high-frequency movement meets the stringent requirements for fine particle screening and helps separate solids from water during wet screening and dewatering.
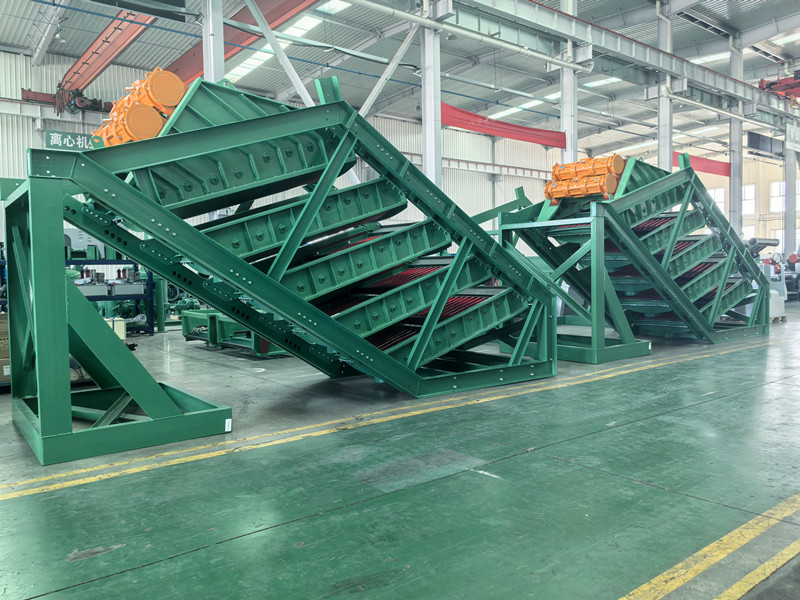
2026.11.11 Stack Vibratring Screeen

By combining high-frequency vibration and multi-layer stacked structure, the high-frequency stack vibrating screen combines the strengths of stack screening and fine screening technology. It is an ideal choice for projects that demand both high screening efficiency and a small installation footprint.

Mining sites differ greatly in material properties, feed conditions and production goals. The flexible 2–5 layer configuration allows customers to customize the machine to match their specific classification and separation needs.

Fine particle screening is a critical link in mineral processing. Accurate classification optimizes downstream beneficiation, while efficient dewatering cuts product moisture and simplifies subsequent handling, stacking and transportation.

As a professional manufacturer of solid-liquid separation and screening equipment, GN Separation keeps innovating to keep pace with the evolving needs of the mining industry. The high-frequency stack vibrating screen is a typical result of our combination of practical engineering design and independent core technology.

This successful supply further proves GN Separation’s strength in fine material screening and mineral processing. Going forward, we will continue to provide customers with durable screening equipment and customized solutions tailored to individual process flows.

Reach out to GN Separation to learn more about our high-frequency stack vibrating screens and other mineral processing equipment.
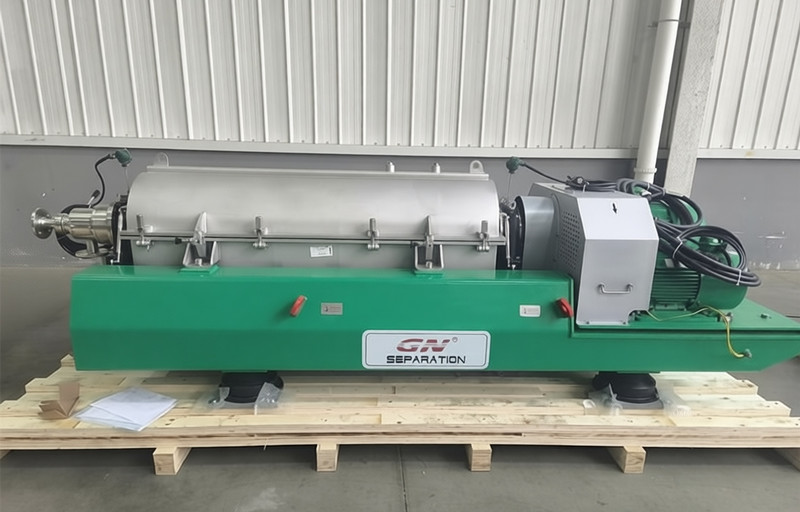
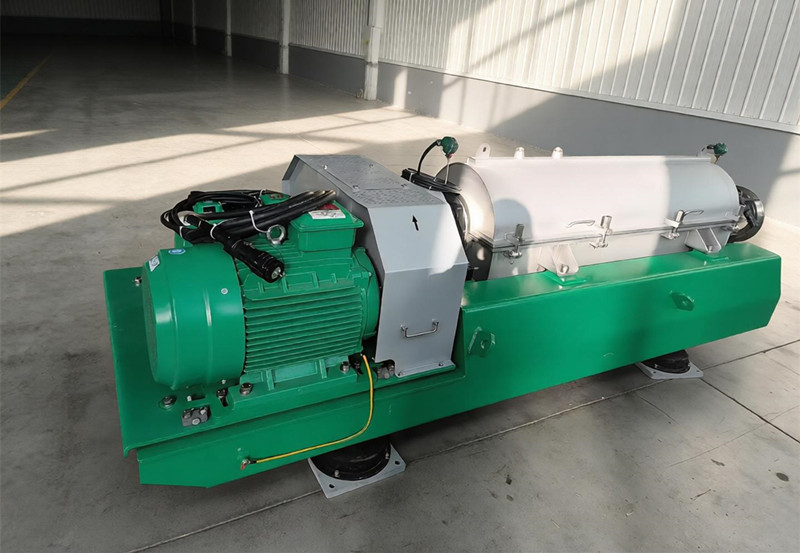
Canola Oil Clarification Decanter Centrifuge for Australia Customer

GN Separation has rolled out a custom decanter centrifuge solution for a canola oil clarification project in Australia. Built specifically for edible oil processing, this system delivers efficient solid-liquid separation while prioritizing hygiene standards, operational flexibility and long-term reliability.

2026.11.05 Canola Oil Clarification Centrifuge

We paid close attention to the centrifuge’s internal design to meet strict food-grade requirements for this Australian client. One standout custom feature is the polished internal screw conveyor. The finely finished screw surface minimizes material sticking and reduces residue buildup inside the machine.

This is a critical advantage for food processing. Any leftover material trapped inside the equipment can degrade over time and compromise oil hygiene. The smooth polished surface also makes routine cleaning much simpler, helping maintain a sanitary production environment.

Another key upgrade is the centripetal pump for discharging clarified liquid. Many conventional centrifuges must be stopped to adjust discharge settings. With our design, operators can tweak the liquid pool depth on the fly, without shutting down the machine.

2026.11.05 Edable Oil Treatment Centrifuge

By adjusting the liquid pool depth, the separation performance can be fine-tuned to match changing feed conditions and production targets. This flexibility comes in handy when the feed has fluctuating solid content or variable process parameters. Less unplanned downtime means smoother continuous production and better overall efficiency.

Beyond these customizations, the decanter centrifuge is engineered for stable, continuous separation. Its compact layout, continuous solids discharge and adjustable operating parameters allow seamless integration into existing edible oil processing lines. Every configuration is tailored to the customer’s process goals, balancing separation efficiency, product quality and ease of use.

GN Separation has years of experience designing and manufacturing industrial decanter centrifuges across food processing, wastewater treatment, oil & gas and mining sectors. We know every project is unique, so we adapt our separation technology to fit real-site operating conditions.

This Australian canola oil clarification project is a great example of our application-first design philosophy. Combining hygienic internal surface treatment and flexible liquid pool adjustment, our custom centrifuge offers the customer a dependable separation solution to support efficient processing and consistent canola oil quality.

5 sets of big bowl decanter centrifuges for overseas tailings slurry separation project

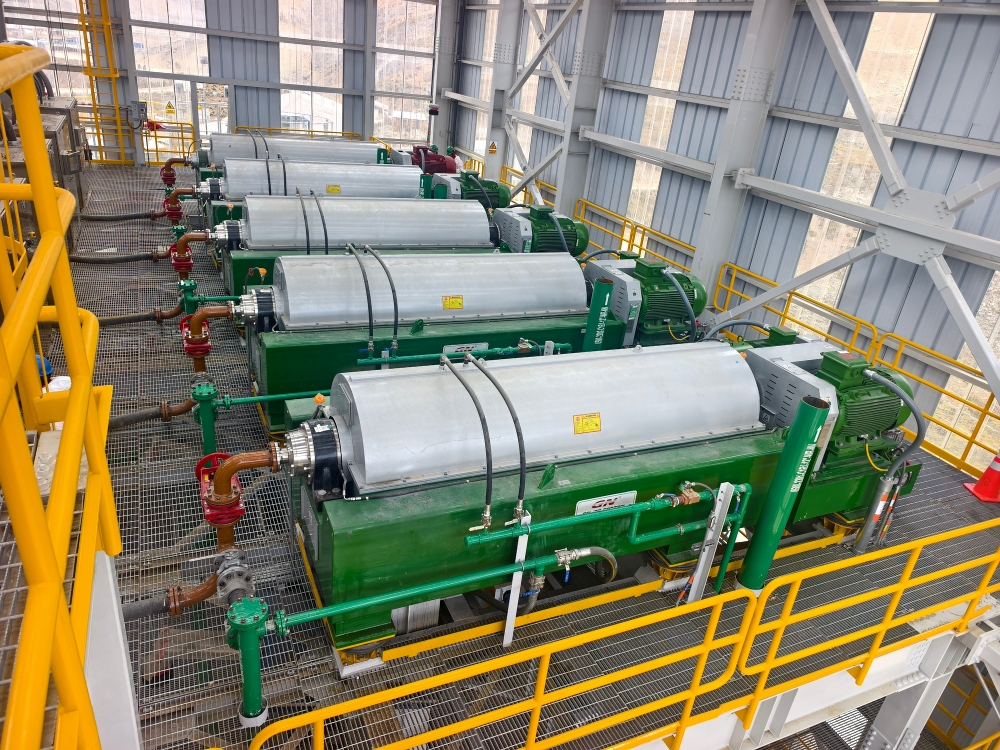
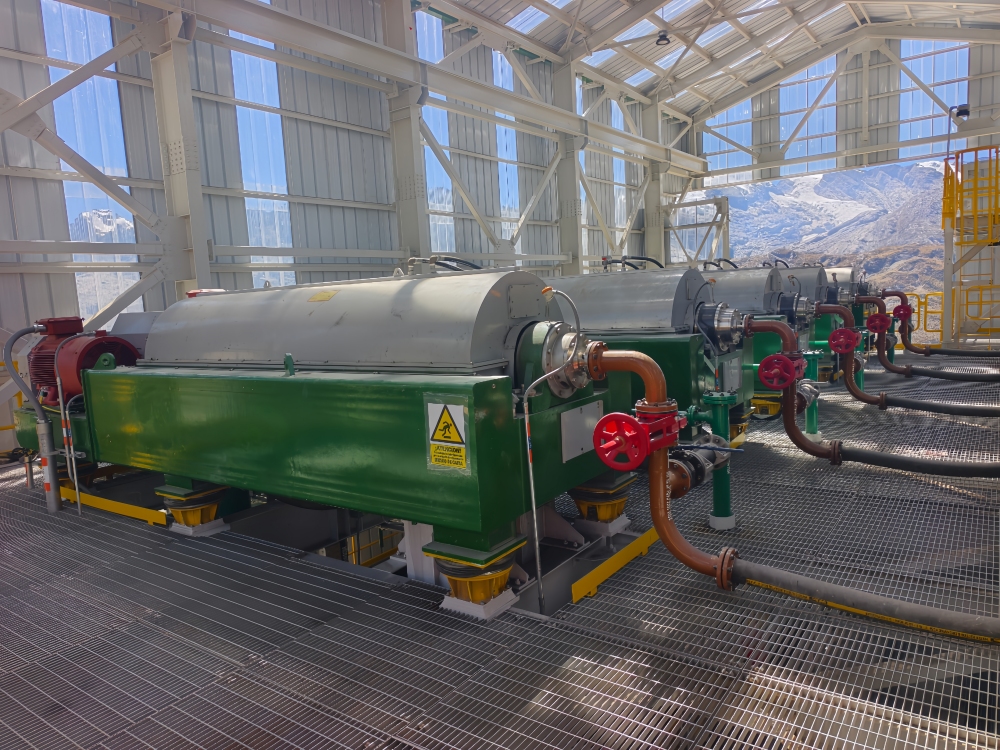
GN Separation has hit a new milestone in the global mining sector: five GNLW764-VFD large-bowl decanter centrifuges have been fully commissioned and are running steadily at an overseas mine tailings treatment facility. Engineered for rigorous slurry separation duties, this set of equipment showcases GN’s strength in developing custom solid-liquid separation solutions suited to harsh mining operating environments.

2026.10.23 Decanter Centrifuge 1

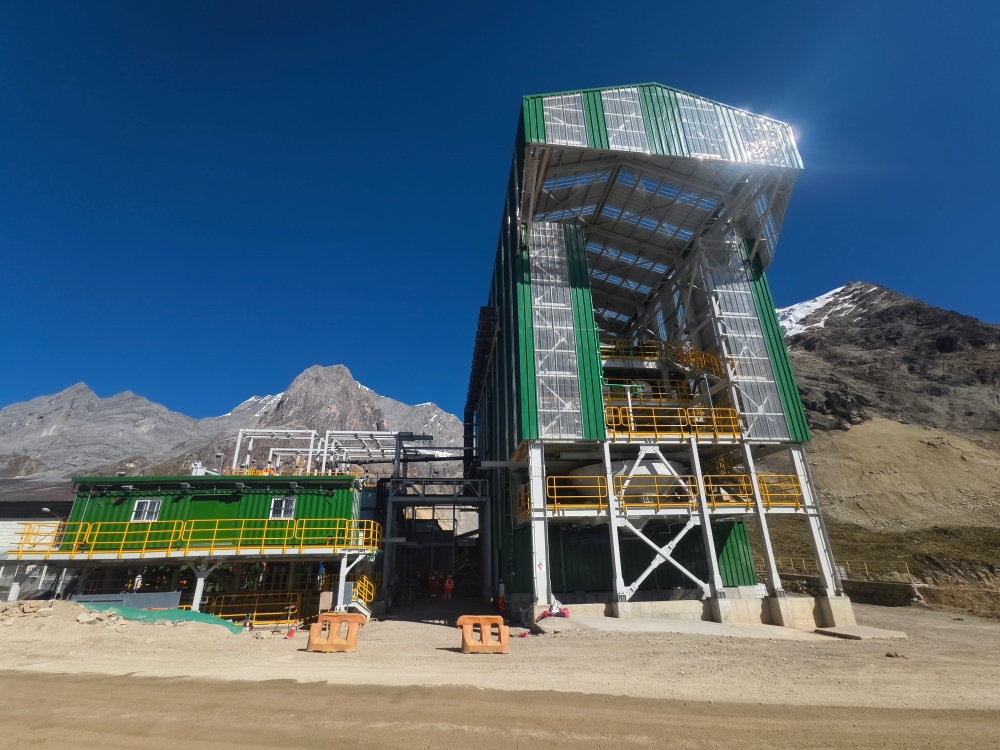
Awarded after an international competitive tender, the project serves a leading mining company. The client prioritized robust machinery capable of processing massive volumes of tailings slurry under tough working conditions. Situated at roughly 4,500 meters above sea level in a high-altitude mining zone, the site posed tough hurdles for equipment performance, operational consistency and wear resistance.

Beyond the extreme elevation, the system must cope with high slurry feed rates and highly abrasive mineral particles, creating heavy loads on the centrifuge’s core parts. Standard off-the-shelf configurations could not satisfy the site’s needs. Long-run reliability, efficient solid-liquid separation and low-maintenance operation were core prerequisites to meet the mine’s production targets.

2026.10.23 Decanter Centrifuge 2

To address these specifications, GN Separation customized the equipment package to match the site’s unique operating parameters. The GNLW764-VFD decanter centrifuge is equipped with a 30-inch large-diameter bowl and variable-frequency drive (VFD) control. The oversized bowl enables high-throughput tailings processing, while variable-speed regulation lets operators tweak process parameters to adapt to fluctuating feed properties and separation targets.

Wear protection was a key focus throughout the design phase. Given the constant erosion from abrasive mineral slurry on critical components, GN adopted targeted wear-resistant structures and upgraded material selections for high-wear zones. These upgrades extend equipment service life and enable uninterrupted operation within harsh mining scenarios.

Instead of rolling out the full fleet at once, the project kicked off with a single test unit delivered to site. This trial centrifuge allowed the customer to assess its real-world performance on location, covering separation efficiency, running stability and long-term production adaptability.

Upon passing on-site testing and performance verification, the customer approved the equipment and placed a follow-up order for four additional identical units. The project was finally scaled up to five GNLW764-VFD decanter centrifuges — a clear testament to how on-site trials and proven performance build client trust.

The complete treatment system comprises the five large-bowl decanter centrifuges, a 6,000-liter automatic chemical dosing skid and matched screw pumps. These units work in tandem to form a unified tailings slurry treatment circuit, realizing continuous feeding, reagent conditioning and solid-liquid separation. This integrated layout streamlines plant operation and facilitates efficient site management.

For mining enterprises, properly managed tailings treatment is critical to boosting process efficiency, controlling solid residues and advancing sustainable water & waste stewardship. By separating solids from slurry, decanter centrifuges cut the volume of material for downstream handling and unlock opportunities for process water recovery and reuse, subject to ore characteristics and overall plant design.

The smooth commissioning of all five centrifuges underscores GN Separation’s capability to fulfill stringent client demands via tailored equipment design, full engineering backing and field performance validation. The whole project journey — from the initial single-unit trial to the finalized five-machine integrated system — illustrates GN’s pragmatic approach to supplying dependable separation equipment for complex overseas mining projects.

2026.10.23 Decanter Centrifuge 3

GN Separation keeps advancing solid-liquid separation technologies for mining, mineral processing and industrial wastewater treatment. By pairing high-capacity decanter centrifuges with application-tailored engineering and matched auxiliary systems, GN supports mining clients worldwide in lifting treatment efficiency, sustaining stable production and complying with increasingly stringent environmental regulations.