GN Separation has rolled out a custom decanter centrifuge solution for a canola oil clarification project in Australia. Built specifically for edible oil processing, this system delivers efficient solid-liquid separation while prioritizing hygiene standards, operational flexibility and long-term reliability.
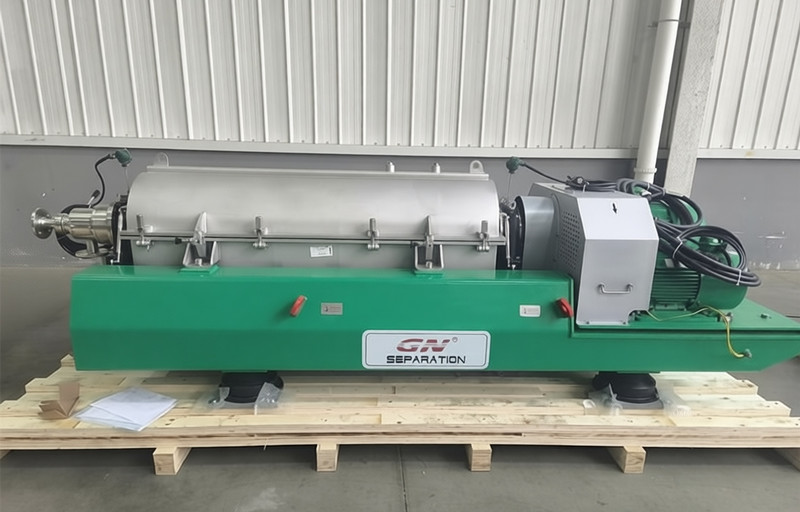
We paid close attention to the centrifuge’s internal design to meet strict food-grade requirements for this Australian client. One standout custom feature is the polished internal screw conveyor. The finely finished screw surface minimizes material sticking and reduces residue buildup inside the machine.
This is a critical advantage for food processing. Any leftover material trapped inside the equipment can degrade over time and compromise oil hygiene. The smooth polished surface also makes routine cleaning much simpler, helping maintain a sanitary production environment.
Another key upgrade is the centripetal pump for discharging clarified liquid. Many conventional centrifuges must be stopped to adjust discharge settings. With our design, operators can tweak the liquid pool depth on the fly, without shutting down the machine.
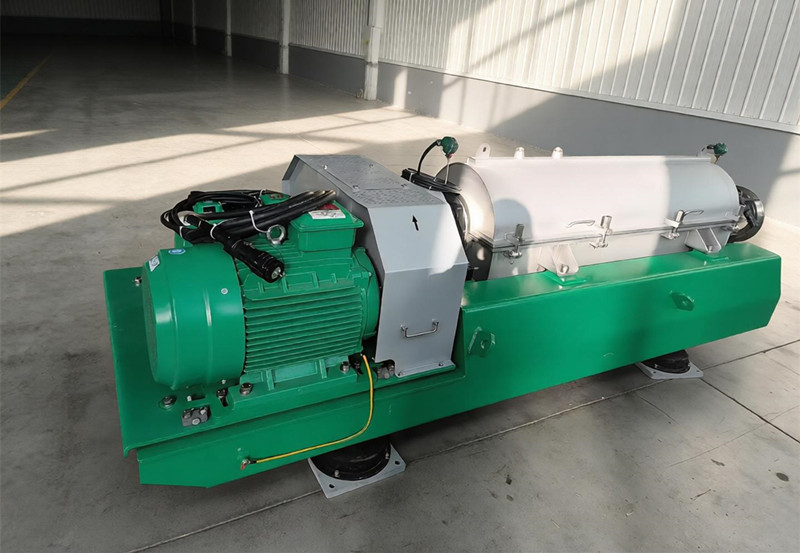
By adjusting the liquid pool depth, the separation performance can be fine-tuned to match changing feed conditions and production targets. This flexibility comes in handy when the feed has fluctuating solid content or variable process parameters. Less unplanned downtime means smoother continuous production and better overall efficiency.
Beyond these customizations, the decanter centrifuge is engineered for stable, continuous separation. Its compact layout, continuous solids discharge and adjustable operating parameters allow seamless integration into existing edible oil processing lines. Every configuration is tailored to the customer’s process goals, balancing separation efficiency, product quality and ease of use.
GN Separation has years of experience designing and manufacturing industrial decanter centrifuges across food processing, wastewater treatment, oil & gas and mining sectors. We know every project is unique, so we adapt our separation technology to fit real-site operating conditions.
This Australian canola oil clarification project is a great example of our application-first design philosophy. Combining hygienic internal surface treatment and flexible liquid pool adjustment, our custom centrifuge offers the customer a dependable separation solution to support efficient processing and consistent canola oil quality.