GN Separation has recently fulfilled a successful equipment delivery, dispatching two sets of GNFG1440 high-frequency vibrating screens to an overseas mining client. The newly commissioned equipment will be officially put into the customer’s mineral processing system, providing professional and high-efficiency solutions for wet screening, fine particle classification and material dewatering. It will effectively streamline the client’s fine-grained ore processing procedures and boost overall production efficiency.
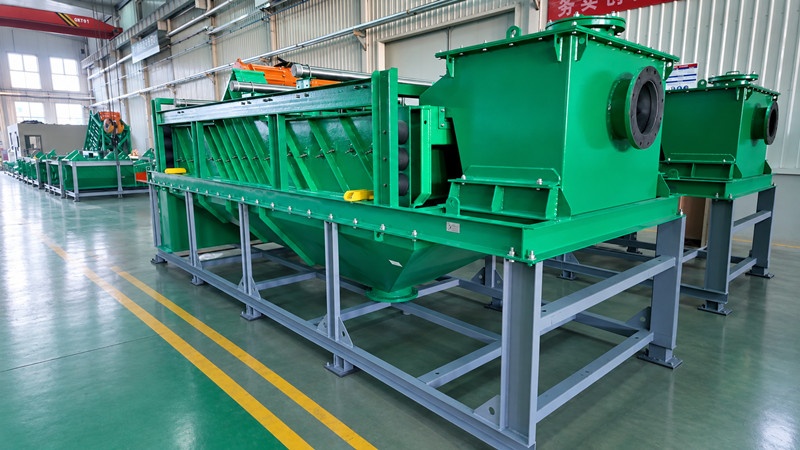
Advanced Resonance Vibration System for Stable Fine Screening
The GNFG series high-frequency fine vibrating screen stands out from conventional screening equipment with its innovative two-degree-of-freedom resonance principle. Powered by dual imported vibration motors as a unified vibration source, the entire machine delivers steady and consistent linear vibration. This sophisticated structural design enables uniform material flow on the screen surface, supports continuous high-frequency screening operation, and perfectly addresses common industry pain points such as fine material adhesion and screen clogging that plague traditional screening equipment.
Compact & Adjustable Structure for Versatile Onsite Adaptability
Engineered with practical onsite application in mind, the GNFG1440 vibrating screen combines a large effective screening area with a compact footprint. It achieves outstanding screening throughput without occupying excessive plant space, maximizing customers’ site space utilization. Equipped with an adjustable screen box angle, the equipment can be flexively calibrated according to different ore properties and production demands, adapting to diverse fine-grained material processing scenarios and realizing customized screening and classification effects.
High Throughput & Energy Efficiency for Continuous Industrial Operation
Featuring a exclusive high-frequency vibration mode, the machine accelerates rapid particle stratification and separation, greatly improving the accuracy and efficiency of wet screening and ore classification. Compared with traditional screening equipment of the same grade, it delivers larger single-unit processing capacity and more stable operational results. Meanwhile, the optimized vibration system minimizes redundant energy consumption, realizing energy-saving and low-cost operation. It is fully qualified for long-term, non-stop industrial mining production, helping clients cut operational costs while maintaining stable production output.
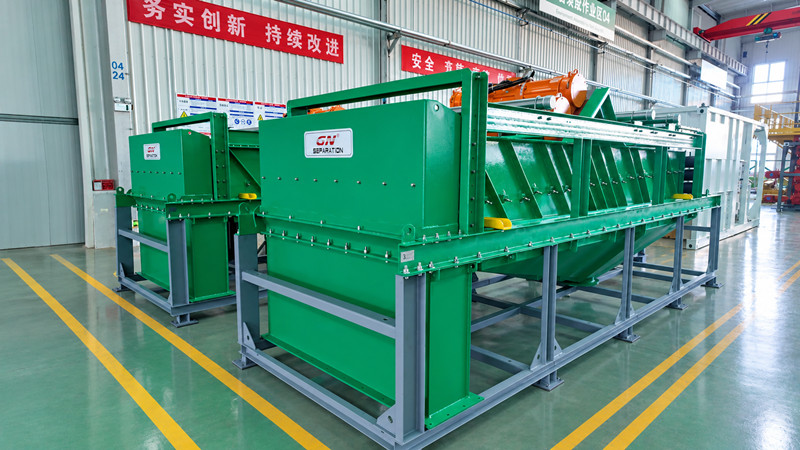
Durable Polyurethane Screen Mesh Lower Maintenance Costs
To tackle the problems of easy screen wear and frequent replacement in fine ore processing, we adopt high-performance polyurethane screen mesh for all GNFG series vibrating screens. Boasting a high opening rate and superior wear and impact resistance, the screen mesh maintains stable and efficient screening performance with low clogging risk in long-term operation. Under conventional working conditions, its average service life can exceed 6 months (varies with material characteristics and working environments), significantly reducing equipment downtime, screen replacement frequency and overall maintenance costs.
Robust & Low-Maintenance Design for Long-Term Stable Operation
Beyond excellent screening performance, the GNFG1440 ore classification vibrating screen features a simplified and robust mechanical structure with low failure rates. The humanized modular design facilitates daily inspection, routine maintenance and component replacement, greatly reducing later operational and maintenance pressure for mining enterprises. It is a highly reliable and cost-effective choice for fine-grained ore screening and dewatering projects.
This successful overseas delivery marks another solid step of GN Separation in the global mining equipment market. Adhering to the concept of high-efficiency fine processing, energy conservation and reliable performance, our high-frequency vibrating screens continue to deliver premium, tailored screening solutions for global mining customers, helping optimize mineral processing workflows and create greater commercial value for end users.