GN Separation has completed the development of a customized Decanter Centrifuge solution for a canola oil clarification application in Australia. The equipment is designed to meet the specific demands of edible oil processing, with a focus on effective solid-liquid separation, hygienic design considerations, and convenient operation.
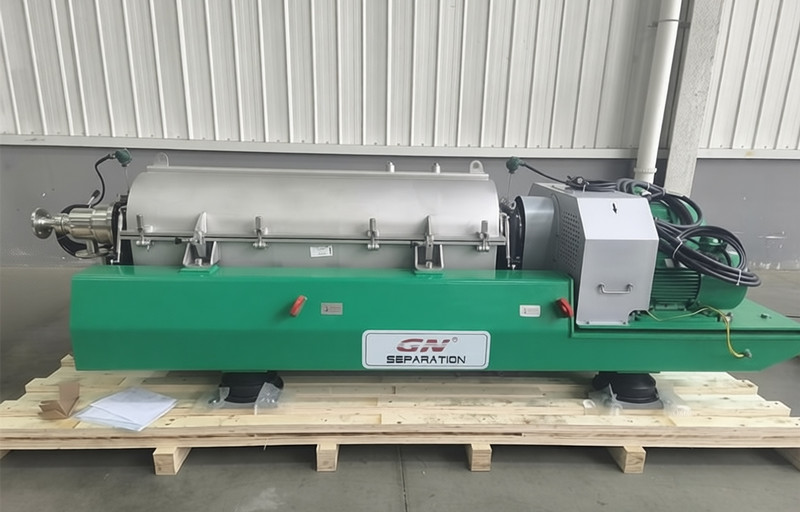
A major consideration in this project was the internal design of the centrifuge. To reduce material buildup and make cleaning easier, GN applied a special polishing treatment to the internal screw conveyor. The smoother screw surface helps minimize material adhesion and the accumulation of residual material during operation. For edible oil processing, this is an important design consideration, as accumulated residues may deteriorate over time and create potential hygiene concerns. The polished finish also supports easier cleaning and maintenance.
The Decanter Centrifuge is also equipped with a centripetal pump for clarified liquid discharge. This configuration allows operators to adjust the liquid pool depth while the machine is running, without having to stop the equipment. Adjusting the pool depth provides greater flexibility in controlling the separation process and adapting to changes in feed characteristics or operating conditions. As a result, operators can optimize the process more conveniently while avoiding unnecessary production interruptions.
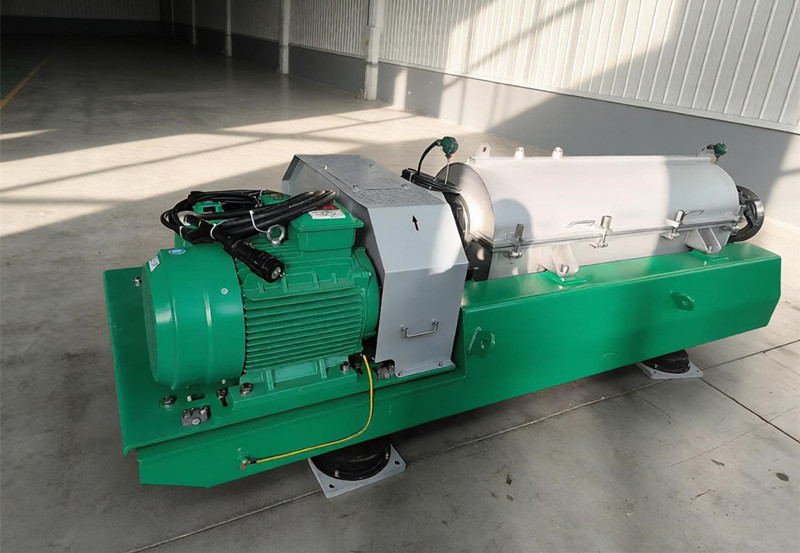
In addition to these application-specific features, the decanter centrifuge is designed for continuous operation, with a compact layout and continuous solids discharge. Its operating parameters can be adjusted to accommodate different process conditions, making it suitable for integration into industrial canola oil processing facilities. The final equipment configuration is selected according to the customer’s process requirements and intended operating conditions.
Decanter centrifuges are widely used in various industries where efficient solid-liquid separation is required. GN Separation provides customized centrifuge solutions for food processing, wastewater treatment, oil and gas, and mining applications. By considering the characteristics of each material and the requirements of each process, GN works to develop equipment configurations that deliver practical value to customers.
The Australian canola oil project is another example of GN’s application-oriented approach to centrifuge design. With a polished internal screw conveyor and an adjustable liquid pool depth during operation, the customized equipment is designed to support hygienic operation, process flexibility, and reliable performance in edible oil clarification.